Purchase Price Is Only One Part of TCO
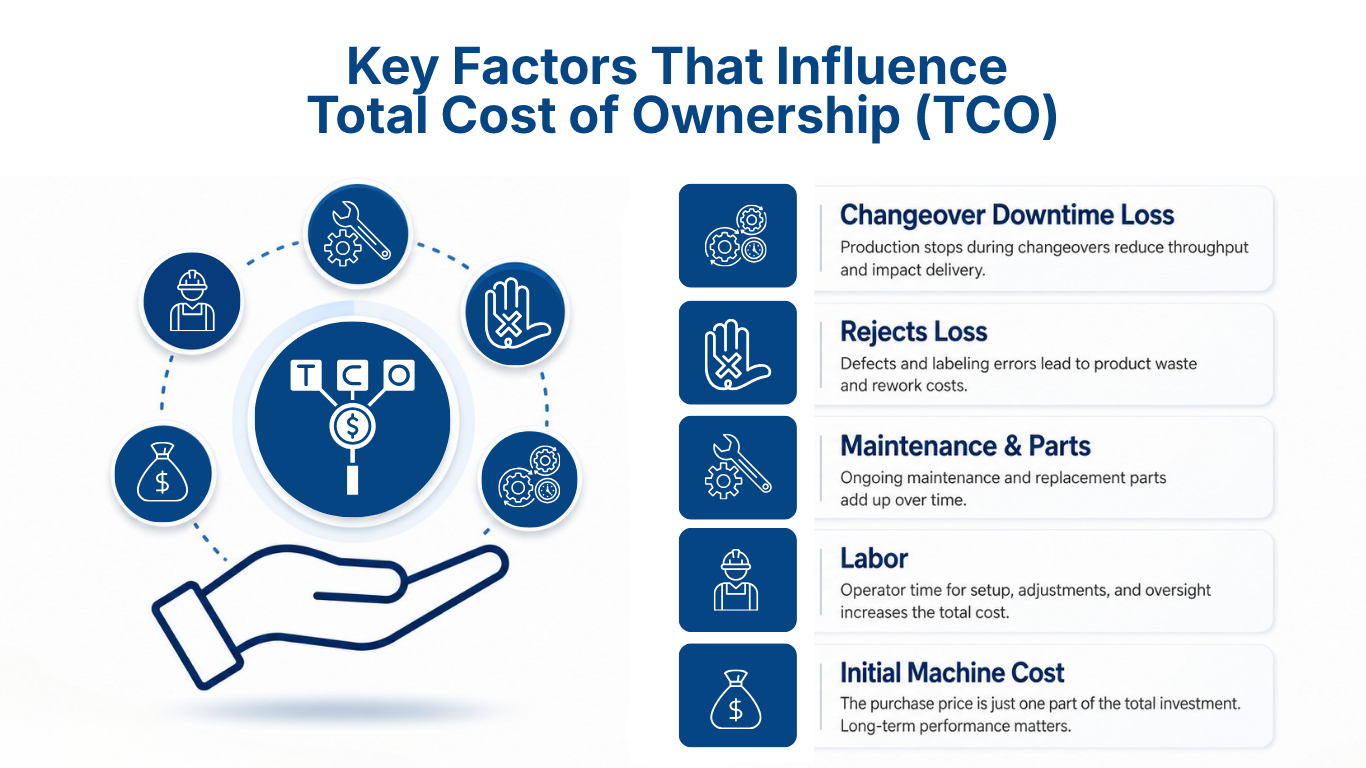
When pharmaceutical manufacturers and CDMOs evaluate labeling equipment, discussions often begin with purchase price. However, the largest costs over the life of a machine are rarely the initial investment. Downtime, changeovers, maintenance, labor, and lost production opportunities often have a much greater impact on Total Cost of Ownership (TCO).
The initial purchase price is only one component of Total Cost of Ownership. Operational losses often account for a significant portion of lifetime costs.
In high-mix pharmaceutical packaging environments, these operational costs can quickly exceed the original equipment investment.
The focus needs to shift from the initial cost of the machine to the long-term costs associated with ownership and operation.
The Cost of Traditional Changeovers
Many packaging operations accept changeovers as unavoidable downtime.
However, every hour spent changing formats is an hour unavailable for production, validation activities, or customer projects.

In a high-mix environment, lost capacity can hinder the company’s ability to respond swiftly to customer requests and accommodate new business opportunities.

Traditional changeovers often require operator intervention, adjustments, and production downtime.
How The SMCL RC-506E Recovers Productive Capacity
One way to reduce operational losses is to simplify changeovers.
The SMCL RC-506E was developed to support high-mix, low-volume pharmaceutical operations by minimizing setup complexity and reducing downtime between product runs.

In this example, the operation performs 67% more changeovers while reducing downtime by nearly 90%.
The result is approximately 53.75 additional productive hours recovered every week.

By eliminating part changes during setup, the RC-506E helps operators move efficiently between different vial sizes, making it easier to support a wider range of products while minimizing downtime.
Recovered Capacity Matters More for CDMOs
For many CDMOs, recovered capacity can be more valuable than direct labor savings.
Every hour recovered from changeovers becomes available for:
- Additional customer projects
- Smaller batch production
- Validation activities
- Urgent commercial demand
- New product introductions
This is why capacity recovery often creates greater business value than simple cost reduction.

In this example, the cumulative value of recovered capacity reaches breakeven in approximately one year and continues to grow throughout the five-year evaluation period.
As Overall Equipment Effectiveness (OEE) improves, a larger percentage of available production time is converted into productive output. By reducing changeover-related downtime, the recovered capacity can be utilized for additional production, customer projects, validation activities, or new product introductions. The more effectively this recovered time is utilized, the faster the initial investment can be recovered.
Over time, the value generated through improved equipment utilization continues to accumulate. Higher OEE accelerates payback by increasing the return generated from existing assets, while the ongoing benefits of recovered capacity continue to reduce total costs and create value well beyond the original payback period.
A Different Way to Evaluate TCO
Traditional equipment evaluations often focus on purchase price.
However, pharmaceutical packaging operations should also consider:
- Downtime
- Changeover efficiency
- Production flexibility
- Recovered capacity
When all relevant factors are considered, TCO becomes a more accurate measure of production and manufacturing capacity.

The true value of a labeling system is not defined solely by its purchase price. The ability to recover productive manufacturing time can play an equally important role in long-term business performance.
Want to see how much capacity your operation could recover?
Our specialists can review your current labeling process, estimate the impact of reducing changeover time, and help identify opportunities to improve productivity, flexibility, and Total Cost of Ownership.
Have questions about automating your labeling process?
Our specialists can help you review your current line,
identify potential inefficiencies, and discuss whether SMCL RC-506E is the right fit for your production environment.
You might also like